About 1000lph Mineral Water Bottling Plant
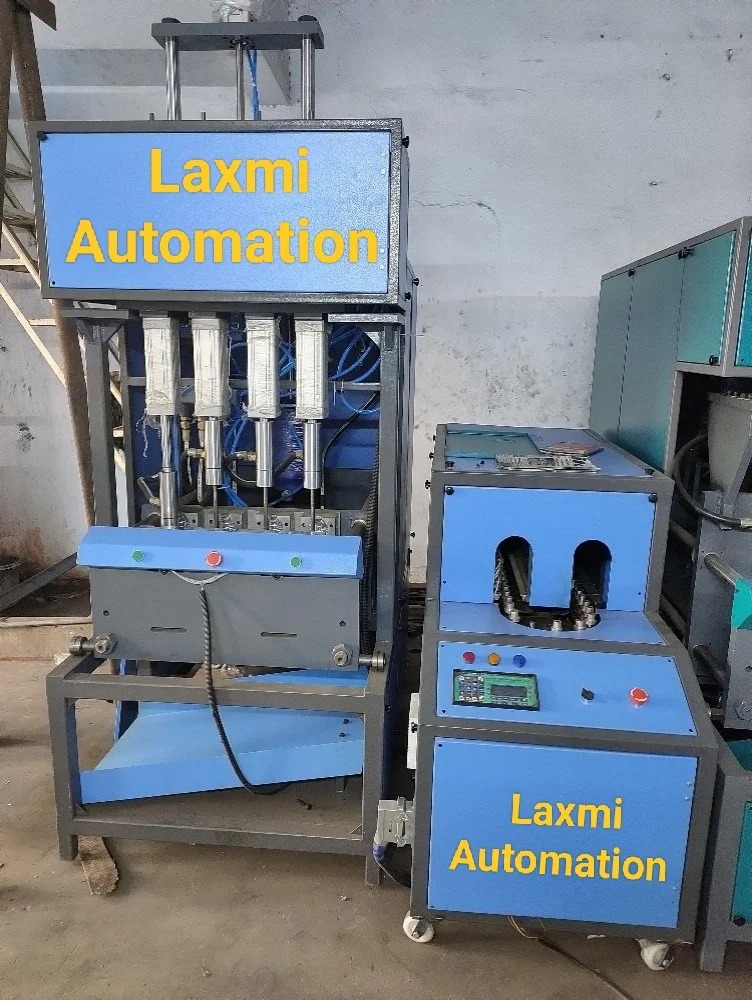
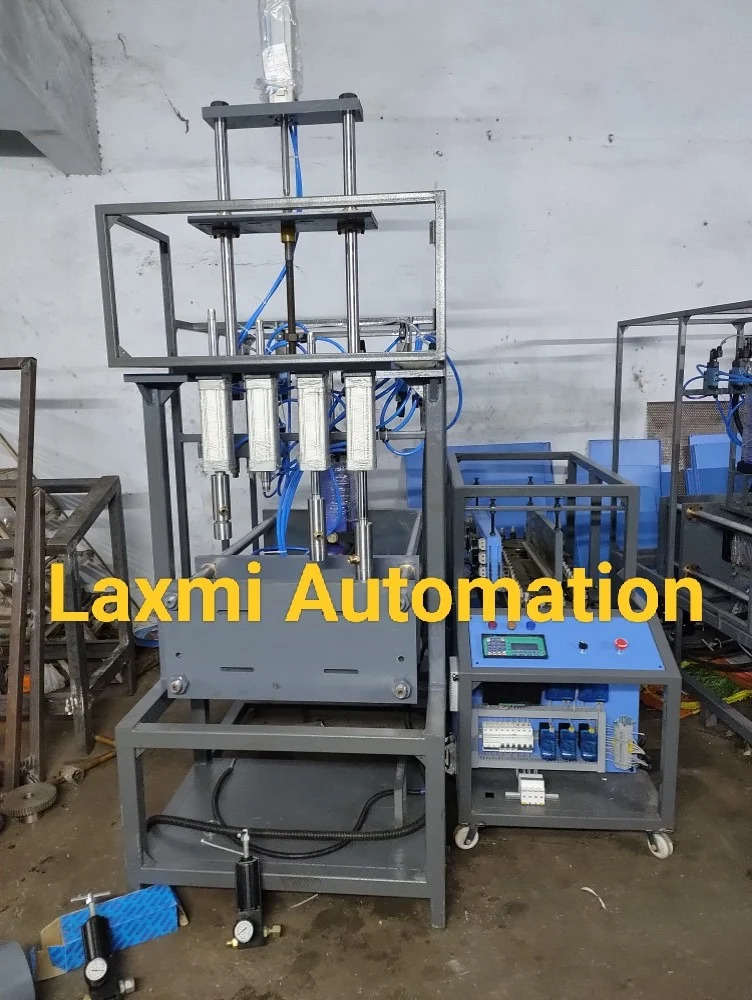
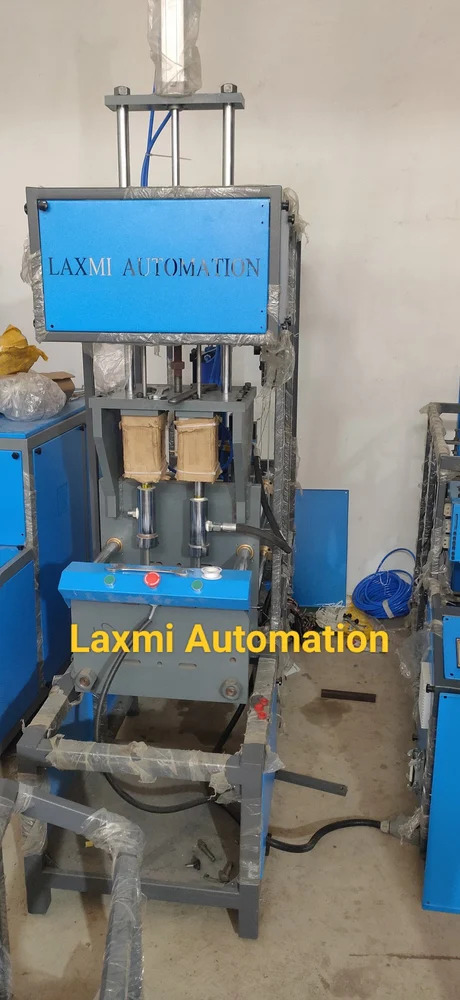
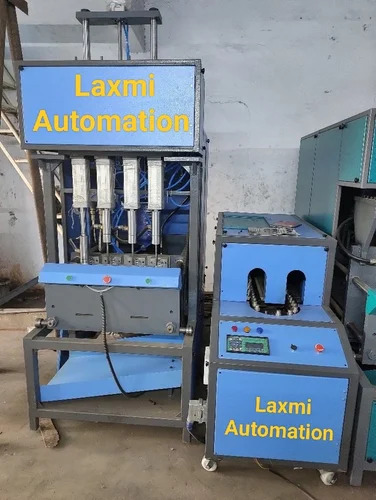
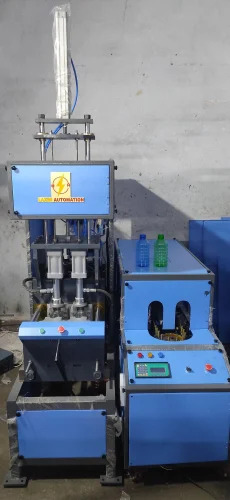
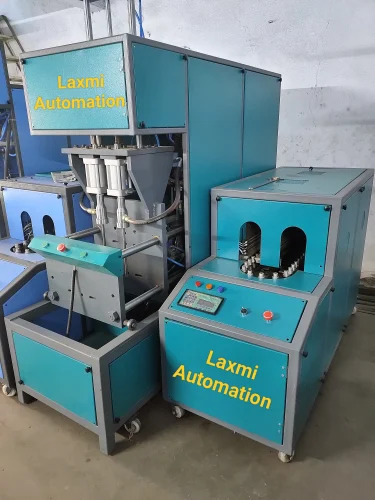
Unlock a towering bargain with our 1000lph Mineral Water Bottling Plant, expertly engineered for ace performance and lasting durability. This deal features a famed mild steel frame, a compact and movable wheeled design, and an advanced digital display for seamless control. The automatic operation, powered by a robust electric drive, ensures efficient production of up to 1000 liters per hour. Highlighted by modern chlorination technology, its powder-coated finish and PET bottle compatibility make it an exceptional choice for bottled water production. An all-in-one plant delivering unmatched value to manufacturers, suppliers, and service providers in India.
Key Uses & Features of the 1000lph Mineral Water Bottling Plant
The 1000lph Mineral Water Bottling Plant excels in bottled water production, making it ideal for commercial beverage businesses and water supply distributors. Key features include an automatic operating system, digital control panel, powder-coated mild steel frame, and PET bottle processing. Its compact structure and movable design ensure flexible installation and operation. The plant's digital display and reliable chlorination technology make it an industry ace for those seeking efficiency, durability, and high output in daily operations.
Sample Availability, Export Markets & Payment Terms
Samples of the 1000lph Mineral Water Bottling Plant are available for clients prior to order completion to ensure satisfaction. Our main export markets include Asia, Africa, the Middle East, and other regions seeking advanced water bottling solutions. Orders are processed promptly, and machines are handed over and shipped once payments are confirmed according to mutually agreed terms. This ensures a smooth transaction and timely delivery of your ace plant to your desired location.
FAQ's of 1000lph Mineral Water Bottling Plant:
Q: How does the automatic operation of the 1000lph Mineral Water Bottling Plant benefit daily production?
A: The plant's automatic operation streamlines the entire bottling process, reducing manual labor while increasing efficiency and consistency. This ensures high output and reliability for commercial water suppliers.
Q: What technology is used for water purification in this bottling plant?
A: The bottling plant utilizes advanced chlorination technology to purify water, meeting quality standards for safe, bottled mineral water production.
Q: When can I expect my 1000lph Mineral Water Bottling Plant to be shipped after order completion?
A: Once your order is completed and payment terms are fulfilled, the plant is promptly handed over to logistics and shipped to your specified address as per our delivery timelines.
Q: Where can this bottling plant be installed effectively?
A: Owing to its compact structure and wheeled, movable design, the plant can be conveniently installed in factories, commercial water bottling units, or warehouses with a suitable single-phase 220 V electric connection.
Q: What are the primary commercial uses of the 1000lph Mineral Water Bottling Plant?
A: It is primarily used for commercial bottled water production, serving beverage manufacturers, water distributors, and suppliers aiming for high-capacity, efficient mineral water packaging.
Q: How user-friendly is the control system of the bottling plant?
A: The digital control panel and display interface are designed for ease of use, enabling operators to manage and monitor proceedings efficiently with minimal training required.
 Send Inquiry




 Send Inquiry


 Send Inquiry
